Elite Steel Elite Steel

Top 10 Ways to Check Stainless Steel Quality Before Buying?

Time:2026-10-24 Author:Sienna
0%

Buying stainless steel is not merely a price comparison. It is a verification process involving grade, dimensions, surface condition, and traceability.

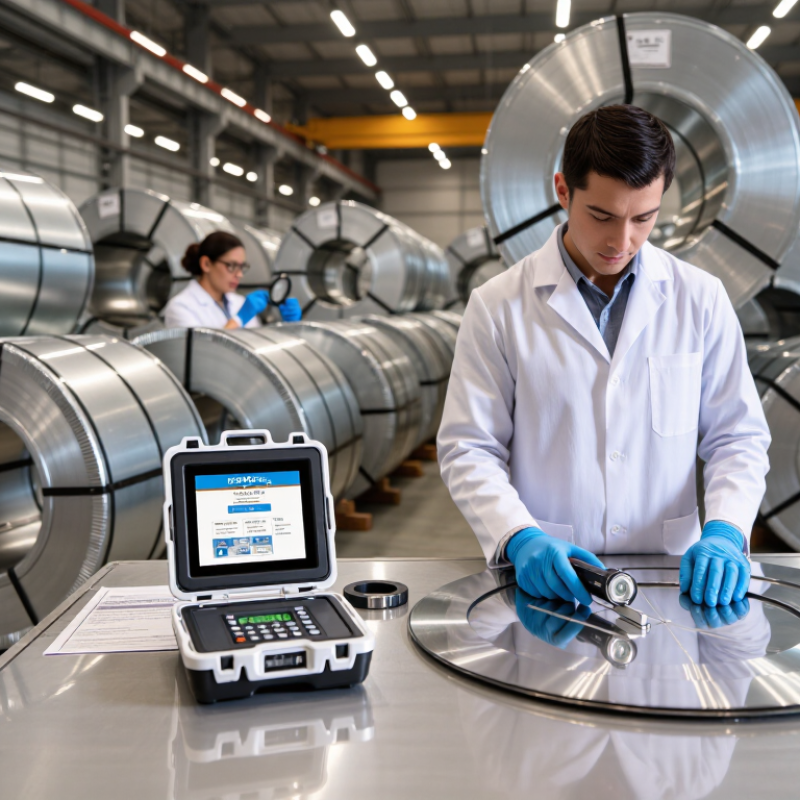
This guide explains How to inspect stainless steel quality before purchase through ten practical checks. You will learn how to review mill certificates, confirm chemical composition, measure thickness, inspect welds, and identify surface defects. Portable X-ray fluorescence testing can help verify nickel, chromium, and molybdenum content. A magnet test may offer a clue, but it cannot confirm the grade alone. That detail is often misunderstood.

Quality expert Dr. Joseph M. Juran offered a useful principle: “Quality does not happen by accident; it must be planned.” His statement fits stainless steel purchasing well. Reliable buyers plan their inspection before the material arrives. They define acceptable tolerances, request heat numbers, and compare certificates with independent test results. They also examine packaging, edge damage, rust stains, scratches, and signs of mixed inventory.

Small details matter. A clean sheet can still have the wrong alloy. A polished surface can hide poor traceability. Even experienced buyers occasionally trust paperwork too quickly. That is worth questioning.

The following checks are practical, not perfect. They cannot replace accredited laboratory testing for critical applications. However, they can reveal many costly problems before payment, fabrication, or installation begins. A careful inspection protects performance, budget, and long-term reliability.
Top 10 Ways to Check Stainless Steel Quality Before Buying?

Verify Grade Chemistry with PMI: 304 vs 316L and 2.0–3.0% Molybdenum

Before buying stainless steel, request a positive material identification (PMI) test on the actual lot. A shiny surface can still mislead. Portable X-ray fluorescence (XRF) quickly measures chromium, nickel, and molybdenum on pipe, sheet, or fittings. For 304, molybdenum is normally absent or present only in small residual amounts. For 316L, the expected molybdenum range is approximately 2.0–3.0%. That difference matters in chloride-rich conditions, where pitting resistance becomes important.

Ask the inspector to clean paint, scale, and oil from several marked areas before testing. Test both ends and a middle section; mixed heats can hide a purchasing error. Compare results with the mill test certificate, heat number, and purchase specification. The certificate is evidence, not proof. A careful buyer keeps photos and records each reading. XRF cannot reliably confirm carbon, so it cannot alone prove the “L” low-carbon designation. Use optical emission spectroscopy, laser-based testing, or an accredited laboratory when carbon content is critical.

Do not reject good stainless steel because a magnet reacts slightly after forming; cold work can cause this response. Likewise, color is a weak quality indicator. I would pause when one spot passes and another fails. That inconsistency may indicate contamination, coating, or different material. A second test is cheaper than replacing corroded equipment.

Check Chromium and Nickel Against ASTM A240 Composition Limits

Before buying stainless steel, compare its chromium and nickel content with the correct ASTM A240 grade requirements. ASTM A240 covers stainless steel plate, sheet, and strip, but limits vary by grade. For example, Type 304 commonly contains 18–20% chromium and 8–10.5% nickel. Type 316 usually contains 16–18% chromium and 10–14% nickel, plus molybdenum. Type 430 generally contains 16–18% chromium and only a small amount of nickel.

Ask for the material test certificate before accepting the shipment. Check the heat number, product grade, chemical analysis, and applicable ASTM specification. An X-ray fluorescence test can provide a fast field screening result. I have found it useful when labels look correct but the metal composition raises questions. Clean the test area first. Paint, scale, and surface contamination can affect readings. Test more than one location when possible.

Chromium supports corrosion resistance. Nickel improves structure and performance in many austenitic grades. However, composition alone does not prove complete quality. Welding condition, surface finish, thickness, and heat treatment may also matter. A quick test can mislead. Portable instruments may struggle with thin sheets or mixed surfaces. When results fall near a specification limit, use an accredited laboratory for confirmation. Keep the certificate and test report together with the purchase records.

Measure Thickness, Flatness, and Tolerances Under ASTM A480

Before buying stainless steel, measure it rather than trusting a polished surface. ASTM A480 provides general requirements for flat-rolled stainless products, including thickness, flatness, and dimensional tolerances. Check the purchase specification and applicable tolerance table carefully. Requirements can change with thickness, width, product form, and ordering conditions.

Use a calibrated micrometer at several points across the sheet. Avoid measuring directly on edges, where burrs may distort readings. Record measurements near the corners and center. One reading is not enough. A sheet may meet the nominal thickness at the center but fall outside tolerance near the sides. For flatness, place the sheet on a stable surface. Use a straightedge and feeler gauge to measure gaps, or follow the inspection method specified for the order. Small waves can become serious during cutting or welding.

Tips: Ask for the material test report and compare its stated dimensions with your measurements. Confirm the gauge, width, length, and flatness limits before accepting delivery. Check whether the surface is clean and free from dents, scratches, and embedded debris. A visual inspection helps, but it cannot prove compliance. I have seen attractive sheets fail a simple thickness check. That is a useful reminder: appearance is evidence, not certainty. Also, inspect your tools before testing. A worn micrometer can create confident but incorrect results.

Top 10 Ways to Check Stainless Steel Quality Before Buying — Measure Thickness, Flatness, and Tolerances Under ASTM A480

Practical pre-purchase inspection checklist for stainless steel plate, sheet, and strip. Example readings are illustrative and must be compared with the ordered grade, product form, dimensions, and applicable ASTM requirements.

No. Quality Check How to Measure Illustrative Inspection Data Acceptance Basis Result
1 Material grade and heat traceability Review the material test report (MTR), heat number, product specification, and marking on the bundle. Confirm that the heat number is traceable from the material to the certificate. Ordered grade: Type 304 stainless steel
Heat number on MTR: H304-26041
Heat number on bundle: H304-26041
The MTR should identify the applicable ASTM product specification, grade, heat analysis, mechanical results, and product form. ASTM A480/A480M provides general requirements; the product specification controls grade-specific requirements. Pass if traceable
2 Chemical composition Verify the MTR against the applicable grade specification. For independent confirmation, use an X-ray fluorescence (XRF) analyzer for alloy screening; use laboratory methods when carbon, nitrogen, or full chemistry is required. Example Type 304 chemistry: Cr 18.2%, Ni 8.1%, Mn 1.2%, Si 0.45%, C 0.035% Compare every element with the applicable ASTM grade specification, such as ASTM A240/A240M for plate, sheet, and strip. XRF is not a complete substitute for laboratory carbon or nitrogen analysis. Compare with grade limits
3 Thickness and thickness variation Measure with a calibrated micrometer at several locations along the length and width, away from burrs, welds, and damaged edges. Record minimum, maximum, and average values. Ordered thickness: 2.00 mm
Readings: 1.98, 1.99, 2.01, 2.02, 2.00 mm
Range: 1.98–2.02 mm
Use the applicable ASTM A480/A480M thickness-tolerance table for the ordered thickness, product form, width, edge condition, and whether the dimension is specified as a minimum or nominal thickness. Do not apply a universal tolerance to every product. Check applicable table
4 Width and length Measure width with a steel rule or calibrated tape at both ends and at the center. Measure length along both edges and through the centerline on cut-to-length material. Ordered sheet: 1,500 × 3,000 mm
Measured width: 1,500.4 mm
Measured lengths: 3,000.8, 3,000.5, 3,000.7 mm
Compare measurements with the ordered size and the applicable ASTM A480/A480M dimensional-tolerance provisions. Tolerances vary by product form, thickness, width, length, and cutting condition. Check order tolerance
5 Flatness Place the sheet on a true reference surface. Use a calibrated straightedge or precision level and measure the greatest gap with feeler gauges at multiple locations. Sheet size: 1,500 × 3,000 mm
Maximum measured gap under a 1,000 mm straightedge: 2.5 mm
Compare the result with the applicable ASTM A480/A480M flatness tolerance for the ordered product. Flatness limits are not one fixed value; they depend on product dimensions, thickness, and specified tolerance category. Check flatness table
6 Edge condition and squareness Visually inspect cut, sheared, or rolled edges. Check diagonal difference for squareness and measure burr height with a microscope or calibrated gauge where edge preparation is critical. Diagonal A: 3,354.1 mm
Diagonal B: 3,354.8 mm
Difference: 0.7 mm
No loose laminations observed
Confirm the ordered edge condition, such as mill edge or cut edge, and compare squareness or edge requirements with the applicable ASTM A480/A480M provisions and purchase order. Record edge condition
7 Surface finish and appearance Inspect both sides under consistent lighting. Check for pits, scale, scratches, roll marks, staining, slivers, dents, and corrosion. For finish-critical work, compare with an agreed reference sample or measure roughness using a calibrated profilometer. Specified finish: No. 2B
Visual result: uniform bright-gray surface; no visible pits or scale
Example Ra reading: 0.32 μm on the tested area
Surface finish designations describe processing and appearance, not a universal roughness value. Confirm the required finish designation and any Ra limit in the purchase order or applicable product specification. Match specified finish
8 Mechanical properties Review the certified tensile test, yield strength, elongation, and hardness results. If retesting is required, use specimens and test methods specified by the applicable ASTM product standard. Illustrative Type 304 annealed result:
Yield strength: 245 MPa
Tensile strength: 610 MPa
Elongation: 52%
Acceptance limits depend on grade and condition. For many stainless sheet and plate products, ASTM A240/A240M is used with ASTM A370 test methods; verify the exact edition and material condition. Compare with grade limits
9 Ultrasonic or internal discontinuity testing When specified for thick plate or critical service, request an ultrasonic examination report and verify calibration, scanning coverage, acceptance level, and test standard. Example report: full plate scan completed
No reportable indications above the specified reference level
Calibration block and sensitivity recorded
Ultrasonic examination is not automatically required for all stainless steel sheet or plate under ASTM A480/A480M. It must be specified by the purchase order or applicable supplementary requirement. Required only when specified
10 Mass, quantity, and documentation review Count sheets or coils, weigh the shipment where practical, and reconcile dimensions, heat numbers, quantity, certificates, packing list, and purchase-order requirements before acceptance. Packing list: 20 sheets
Physical count: 20 sheets
Nominal calculated mass: 1,413 kg
Scale reading: 1,421 kg
Use the material density and ordered dimensions for an estimate only; actual mass can vary with thickness, width, length, trimming, and tolerances. Documentation must match the supplied material and heat numbers. Reconcile before payment

Important: ASTM A480/A480M contains general requirements and dimensional provisions for flat-rolled stainless and heat-resisting steel products. Always use the applicable product specification, ordered grade, product form, tolerance category, and edition identified in the purchase order. The numerical readings above are sample inspection data, not universal acceptance limits.

Inspect Surface Finish Using Ra Values: 2B, BA, No. 4, and No. 8

A stainless steel surface can look flawless under warehouse lighting and still fail a finish specification. Check its Ra value with a calibrated roughness tester, measured in micrometres. Ra describes average surface roughness, not the complete surface condition.

Typical 2B sheet often measures around 0.3–0.6 μm Ra, while BA is usually smoother, commonly near 0.1–0.3 μm. No. 4 has visible directional lines and may range from 0.4–1.0 μm. No. 8 aims for a mirror appearance, often below 0.1 μm, but reflections can hide fine defects. These ranges vary with production methods and applicable standards.

Ra alone is not enough. Inspect for pits, scratches, roll marks, waviness, and inconsistent grain direction. I have seen attractive samples that failed under angled light. Appearance can deceive.

Tips: Request the finish standard, test report, and measuring direction before buying. Measure several areas, including the center and edges. Keep the probe clean and use a recent calibration record. If the supplier provides only one Ra reading, ask why. One measurement can mislead. Also compare the sample with the promised finish under bright, angled lighting. A No. 4 finish should show consistent brushing, while a No. 8 finish should reflect evenly without cloudy patches. Samples may not represent the entire batch, so random inspection remains important.

Confirm Corrosion Resistance Through ASTM G48 and Passivation Records

Before buying stainless steel, request an ASTM G48 corrosion test report, not only a polished certificate. ASTM G48 Method A exposes specimens to ferric chloride and measures pitting resistance under controlled conditions. The report should show the alloy grade, test temperature, exposure time, specimen location, surface finish, and pit inspection method. A 24-hour exposure is common, but acceptance limits depend on the project specification. Higher critical pitting temperatures generally indicate stronger resistance, although results are not directly interchangeable between laboratories.

Ask for passivation records linked to the exact production lot. Useful records include the treatment standard, bath chemistry, temperature, contact time, rinsing method, and final inspection results. ASTM A967 covers chemical passivation treatments and verification practices for stainless steel parts. Look for free-iron testing, water-break inspection, or copper sulfate testing where appropriate. A vague statement saying “passivated” is weak evidence.

The NACE IMPACT study estimated global corrosion costs at about 3.4% of global GDP, showing why small documentation gaps deserve attention. Still, a clean report can hide poor sampling. Request photographs of tested surfaces and confirm laboratory accreditation. Review heat tint, scratches, and weld areas separately. Passivation cannot repair incorrect alloy selection or severe contamination. I have seen attractive surfaces fail quickly near welds. That detail is easy to miss.񎟋

Top 10 Ways to Check Stainless Steel Quality Before Buying

Preliminary chemistry screening can help distinguish common stainless-steel grades. The ranges below reflect commonly specified ASTM A240 composition limits for 304 and 316 stainless steel sheet and plate. Chemistry alone does not prove corrosion resistance: request ASTM G48 Method A or Method B test results and verify the passivation record, including the treatment method, date, lot traceability, and inspection results.

The molybdenum range in 316 stainless steel supports improved resistance to localized pitting compared with 304, but actual performance depends on composition, surface condition, fabrication, and exposure conditions. ASTM G48 testing and complete passivation documentation should be reviewed before purchase.

FAQS

Which chromium and nickel levels are common for Type 304 stainless steel?

Type 304 commonly contains 18–20% chromium and 8–10.5% nickel. Check the exact grade limits before acceptance.

How does Type 316 differ from Type 304?

Type 316 usually contains 16–18% chromium and 10–14% nickel. It also includes molybdenum for improved resistance in demanding environments.

What documents should I request before accepting stainless steel?

Request the material test certificate and purchase records. Confirm the heat number, grade, chemical analysis, and applicable specification.

Can portable X-ray fluorescence testing confirm the alloy completely?

It provides fast screening, but it does not prove complete quality. Clean paint, scale, and contamination from the test area first.

What can cause an incorrect X-ray fluorescence reading?

Thin sheets and mixed surfaces can confuse portable instruments. Test several locations when possible. Near-limit results need laboratory confirmation.

What should an ASTM G48 corrosion report include?

It should identify the grade, temperature, exposure time, specimen location, and surface finish. It should also explain pit inspection methods.

Does a 24-hour corrosion test guarantee field performance?

No. Acceptance limits depend on the project specification. Sampling, welding, scratches, and heat tint can change real performance.

What evidence shows that passivation was properly completed?

Request records for treatment chemistry, temperature, contact time, rinsing, and final inspection. Free-iron or water-break testing adds useful evidence.

Can passivation fix the wrong alloy or severe contamination?

No. Passivation cannot correct incorrect alloy selection. It also cannot reliably repair deep scratches or heavy weld contamination.

What mistake is easy to make during stainless steel inspection?

Trusting a polished surface too quickly. Attractive metal may still fail near welds or contain incomplete documentation. I might overlook that.

Conclusion

How to inspect stainless steel quality before purchase starts with verifying the material’s actual grade and chemical composition. Positive Material Identification (PMI) can help distinguish 304 from 316L, while confirming chromium, nickel, and, for 316L, approximately 2.0–3.0% molybdenum. Compare the test results with the applicable ASTM A240 composition limits, and request traceable mill certificates or inspection reports for additional confidence.

Physical condition is equally important. Measure sheet or plate thickness, flatness, and dimensional tolerances according to ASTM A480 requirements. Examine the surface finish and relate its appearance to the specified Ra value, whether it is 2B, BA, No. 4, or No. 8. Finally, review corrosion-resistance evidence, such as ASTM G48 test results and passivation records, to confirm that the material and finishing process meet the intended service conditions. A documented, multi-step inspection can reduce quality risks and support a more reliable purchasing decision.
Sienna

Sienna

Sienna is a skilled marketing professional with a deep expertise in our company’s core products and services. With a passion for innovation and detail, she plays a pivotal role in crafting insightful blog posts that not only highlight the unique features of our offerings but also provide valuable......